What causes liquid slugging in refrigeration compressors?
What causes liquid slugging in refrigeration compressors?
A sudden knock, sharp vibration, or unexpected trip can signal liquid slugging in refrigeration compressors: liquid refrigerant or oil reaches the compression chamber in a quantity the machine cannot safely handle. Replacing damaged valves or pistons may restore operation, but it does not explain why the liquid arrived. The usual causes are evaporator floodback, off-cycle refrigerant migration, unstable expansion control, and poor startup or defrost sequencing. The useful question is not simply “Was liquid present?” It is “Where did it collect, and what operating event carried it into the compressor?”
Separate slugging from floodback and a noisy compressor
Liquid slugging is a mechanical event. Unlike vapor, liquid is effectively incompressible under normal compressor operating conditions. When too much enters a compression pocket, pressure and mechanical loads can rise abruptly. Reciprocating machines may suffer broken valve components, damaged pistons, or bent connecting rods. Scroll and screw compressors have different failure mechanisms and liquid tolerances, but they are not automatically protected against excessive liquid ingestion.
Floodback means liquid refrigerant returns through the suction line during operation. It can dilute oil and damage bearings without producing an obvious slugging event. Refrigerant migration happens while the compressor is stopped and can create a dangerous startup condition later. These terms describe different parts of the failure sequence; treating them as interchangeable makes troubleshooting less precise.
Knocking alone is not proof. Loose mounts, damaged valves, worn bearings, or piping contact can sound similar. If violent knocking or abnormal vibration begins, stop the machine through the approved site procedure rather than repeatedly resetting it to reproduce the sound. Isolate energy before inspection, and follow refrigerant-specific safety requirements.
When the evaporator cannot finish boiling the refrigerant
In a direct-expansion system, the evaporator should absorb enough heat to vaporize the incoming refrigerant and provide the outlet superheat required by the design. Floodback develops when refrigerant feed exceeds the heat available to evaporate it. That imbalance can come from excessive feed, insufficient load, or both.
Consider an air cooler after its coil has iced heavily. The expansion valve may still admit refrigerant, but restricted airflow reduces heat transfer. Failed fans, blocked filters, and obstructed product stacking can produce the same mismatch. On a process chiller, the equivalent checks are liquid flow, pump operation, strainer condition, bypass position, and sudden changes in process demand.
This is why adjusting the expansion valve before checking the load side is often the wrong move. A valve adjustment can hide the symptom at one operating point while leaving the real problem untouched. Restore the intended airflow or process flow, then assess refrigerant control under representative conditions.
Expansion control can be wrong without a failed valve
A thermostatic expansion valve may overfeed because its sensing bulb is loose, poorly positioned, or influenced by surrounding heat. An external equalizer connection can also give misleading pressure feedback if installed incorrectly. Electronic expansion valves introduce other possibilities: inaccurate temperature sensors, incorrect pressure-transducer scaling, unsuitable control settings, or a valve that does not track its command.
Check the entire measurement chain before condemning the valve. Compare controller readings with reliable field instruments, inspect sensor mounting, and observe valve response during load changes. An oversized valve may hunt at low load even though it controls acceptably near full capacity. The replacement decision should reflect the actual operating range, not just the original nominal duty.
Flooded evaporators and pumped-recirculation systems require a different diagnosis. Liquid is expected in parts of those circuits. The relevant questions concern separator level control, vapor disengagement, return flow, and carryover into the compressor suction—not whether the evaporator outlet meets a direct-expansion superheat target.
A quiet shutdown can set up a violent restart
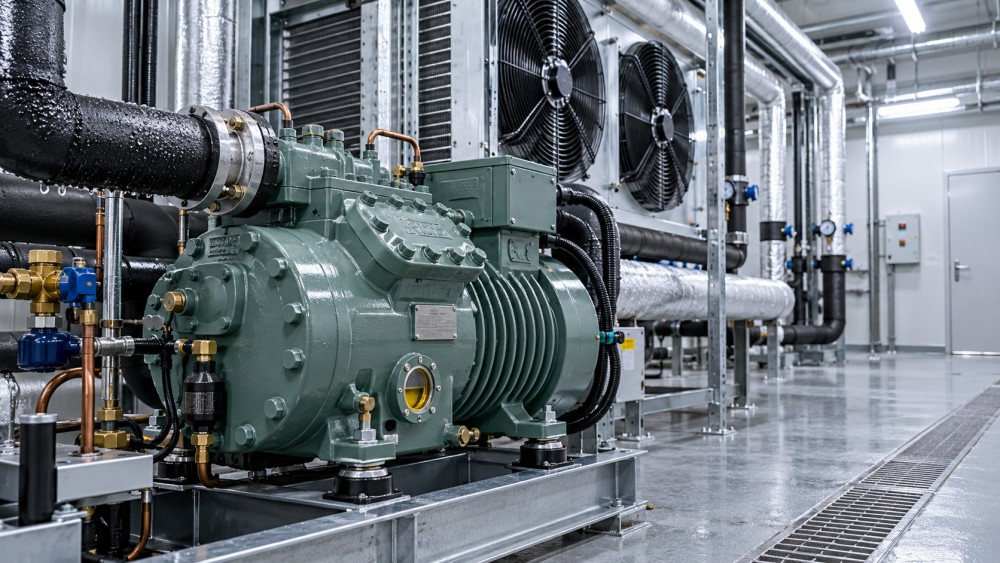
Off-cycle refrigerant migration is particularly easy to miss because running conditions may look acceptable after the system settles. During shutdown, refrigerant can migrate toward colder parts of the system, including the compressor, and dissolve in its oil. A compressor in a cold machinery space may therefore accumulate refrigerant while the evaporator remains warmer.
At startup, the crankcase pressure falls. Refrigerant dissolved in the oil can flash into vapor, causing foaming and carrying oil out of the sump. Depending on the compressor and liquid distribution, this can contribute to liquid ingestion, lubrication loss, or both. A sight glass that suddenly fills with foam is a warning, not a diagnosis by itself.
Check whether the crankcase heater is actually energized when required and whether it performs according to the compressor manufacturer’s instructions. A heater can have electrical continuity yet still provide inadequate heating because of installation problems or operating conditions. After an extended shutdown or loss of power, observe the specified preheating period; there is no universal waiting time suitable for every compressor.
Where the design uses pump-down control, verify the liquid-line solenoid, pressure control, and complete shutdown sequence. A leaking solenoid can allow refrigerant to continue entering the low side. Do not add pump-down indiscriminately: some compressor and system arrangements need different migration protection, and repeated cycling can introduce additional problems.
Look closely at defrost, staging, and oil return
A failure that occurs immediately after defrost deserves a different investigation from one that follows an overnight shutdown. Hot-gas defrost changes refrigerant distribution and pressure throughout the affected circuit. Inadequate drainage, incorrect valve sequencing, or an abrupt return to refrigeration can send retained liquid toward the suction header. Review the actual sequence and timestamps rather than assuming the programmed sequence occurred correctly.
Capacity staging also matters. When compressors unload or cycle off, suction-line velocity may become too low to transport oil reliably. Oil can collect in evaporators, risers, or traps and then return rapidly when capacity increases. That oil surge can itself create a liquid-loading problem. Adding more oil because the sight glass looks low may make the eventual return worse.
A suction accumulator can intercept returning liquid, but it is not a cure for uncontrolled overfeeding. Its usable capacity, pressure drop, oil-return arrangement, and suitability for the refrigerant must match the application. An undersized accumulator can be overwhelmed; a restricted oil-return passage can create a separate lubrication problem. Likewise, oil-injected screw compressors deliberately admit controlled oil flow, but that does not make an uncontrolled oil or refrigerant surge acceptable.
Use the timing of the event to narrow the checks
Before opening the system, record when the symptom appears. A short trend covering the transition often tells more than a complete set of readings taken twenty minutes afterward.
- After a long shutdown: investigate migration, crankcase heating, liquid-line isolation, and refrigerant accumulation.
- During low-load operation: check minimum evaporator flow, valve stability, capacity-control interaction, and suction-line oil transport.
- Immediately after defrost: examine drainage, pressure equalization, valve timing, and separator behavior where applicable.
- After compressor staging or a rapid load increase: investigate stored oil or liquid returning from piping and evaporators.
- After service work: verify refrigerant charge by the approved method, valve positions, sensor reconnection, and the restored control configuration.
For direct-expansion circuits, measure suction pressure and line temperature at corresponding locations. Evaporator outlet superheat and compressor inlet superheat answer different questions; pressure drop and heat gain along the suction line can make them differ. Use the correct refrigerant pressure-temperature relationship, including dew-point values for superheat calculations with zeotropic blends.
Do not apply a universal superheat setting. Acceptable values depend on compressor requirements, evaporator design, refrigerant, and operating envelope. A positive average reading also does not exclude intermittent liquid carryover: a slow sensor may miss a short transient, and a common suction-header measurement may conceal one overfeeding branch.
Frost on a suction line is similarly inconclusive. It indicates a cold surface exposed to moisture, not necessarily liquid inside the pipe. Combine temperature and pressure readings with load conditions, oil behavior, controller trends, and inspection findings. Keep pressure instruments and procedures appropriate to the refrigerant and applicable local requirements.
Repair the liquid path before returning the compressor to service
If damage is suspected, follow the manufacturer’s inspection procedure and assess contamination, oil condition, and lubrication components as well as the visibly broken parts. Mechanical fragments and degraded oil can threaten a replacement compressor. The required cleanup depends on the failure; a mechanical slugging event should not automatically be treated as an electrical burnout.
The practical repair scope may include restoring evaporator flow, correcting sensor installation, repairing a leaking solenoid, revising defrost timing, or reviewing accumulator and piping design. Record what changed and why. This links equipment maintenance to actual process duty—the distinction between rated performance and site operation that matters when evaluating industrial equipment and its lifetime cost.
Before closing the job, verify operation through the condition that caused concern: low load, restart, defrost recovery, or staging. Do not deliberately recreate a damaging event; use controlled commissioning within manufacturer limits. A quiet compressor at steady full load is encouraging, but the repair is not proven until the original route for liquid entry has been identified and corrected.
Related News
- Is an IE4 Motor Upgrade Worth It for a Mostly Part-Load Compressor?Oct 28, 2026
- Are Butterfly Valves Suitable for Isolating Factory Compressed Air Mains?Oct 28, 2026
- How Do You Calculate Globe Valve Pressure Drop in Cooling Water Lines?Oct 28, 2026
- How Do You Calculate Air-Source Heat Pump Payback for a Factory?Oct 28, 2026
- How Do You Calculate a Compressor Cooling Pump's Lifecycle Cost?Oct 28, 2026
- How Do You Size a Cooling Tower for a Compressor?Oct 28, 2026